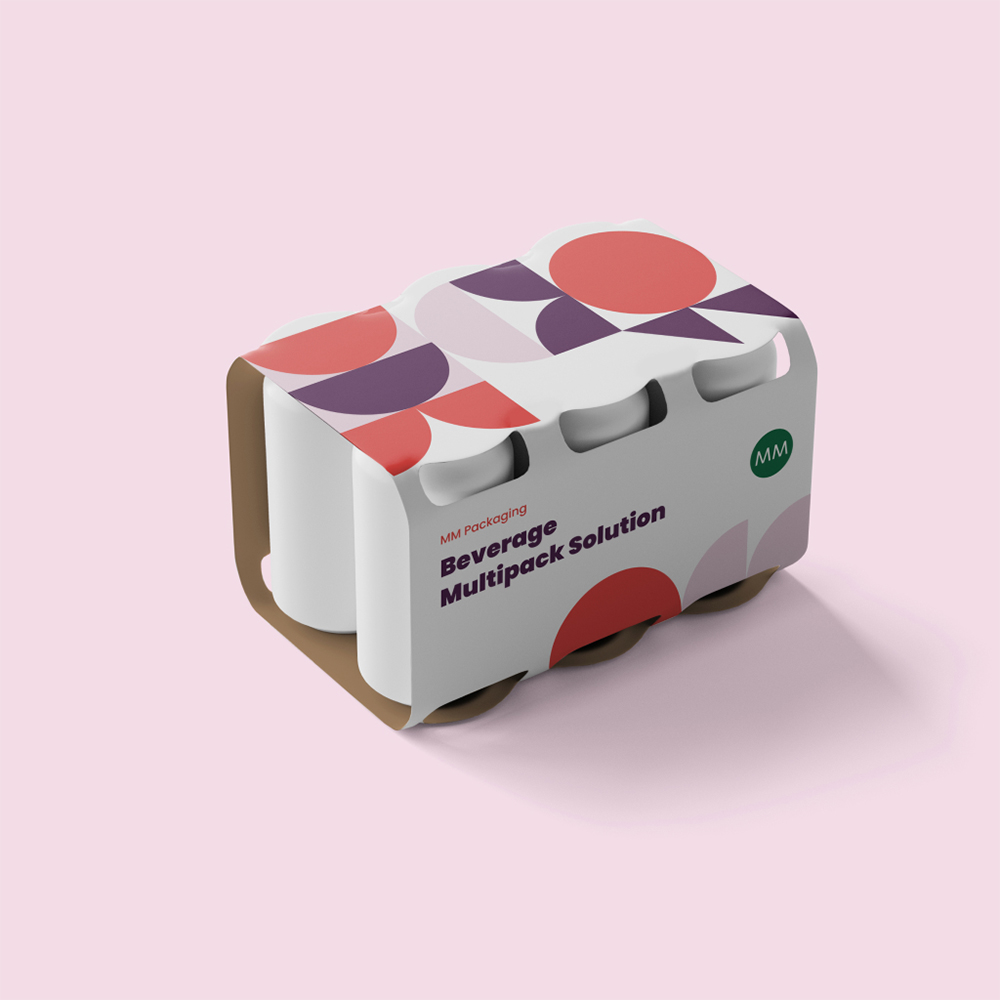
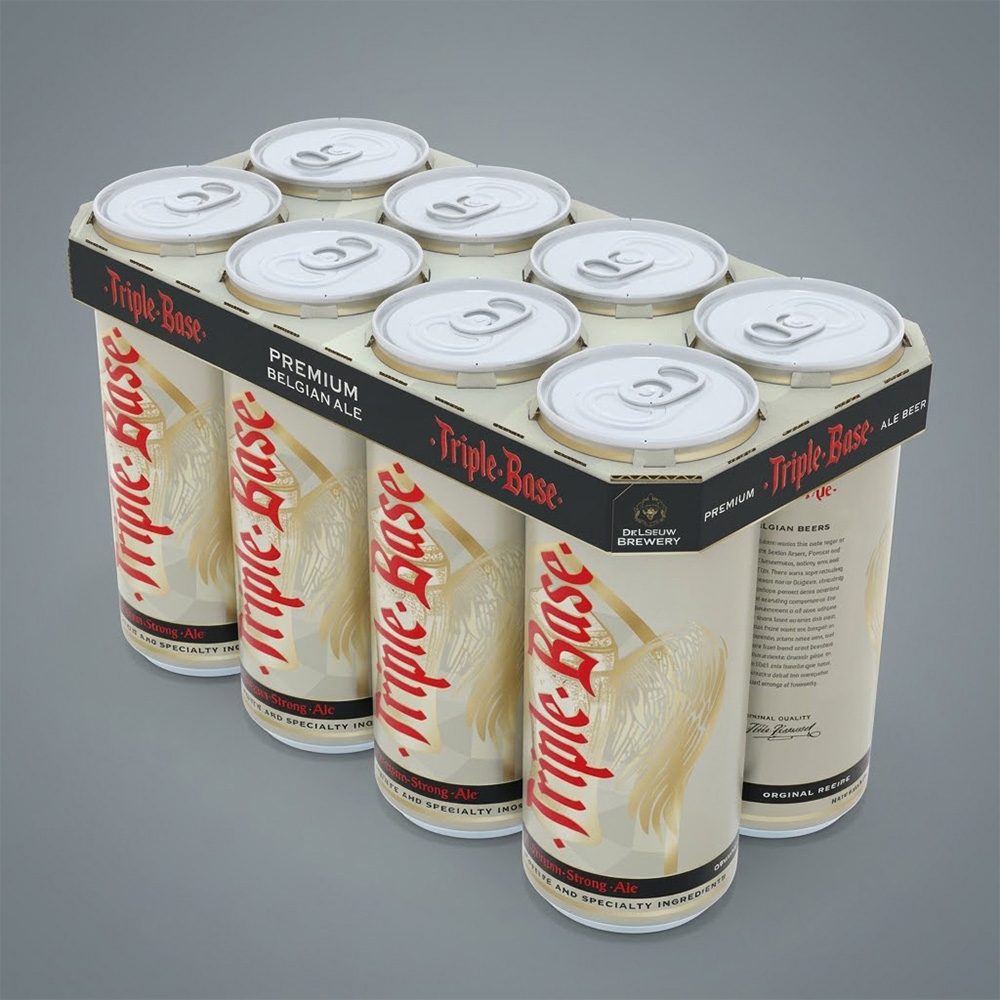
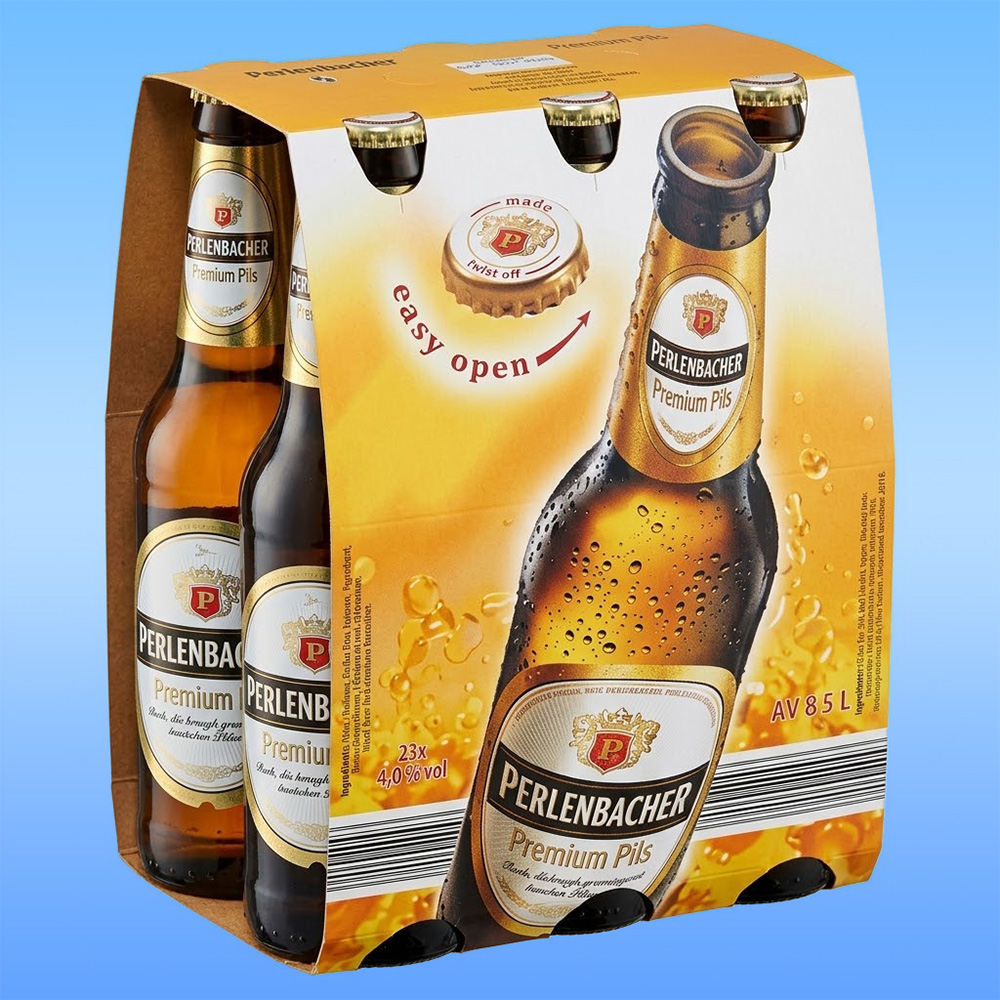
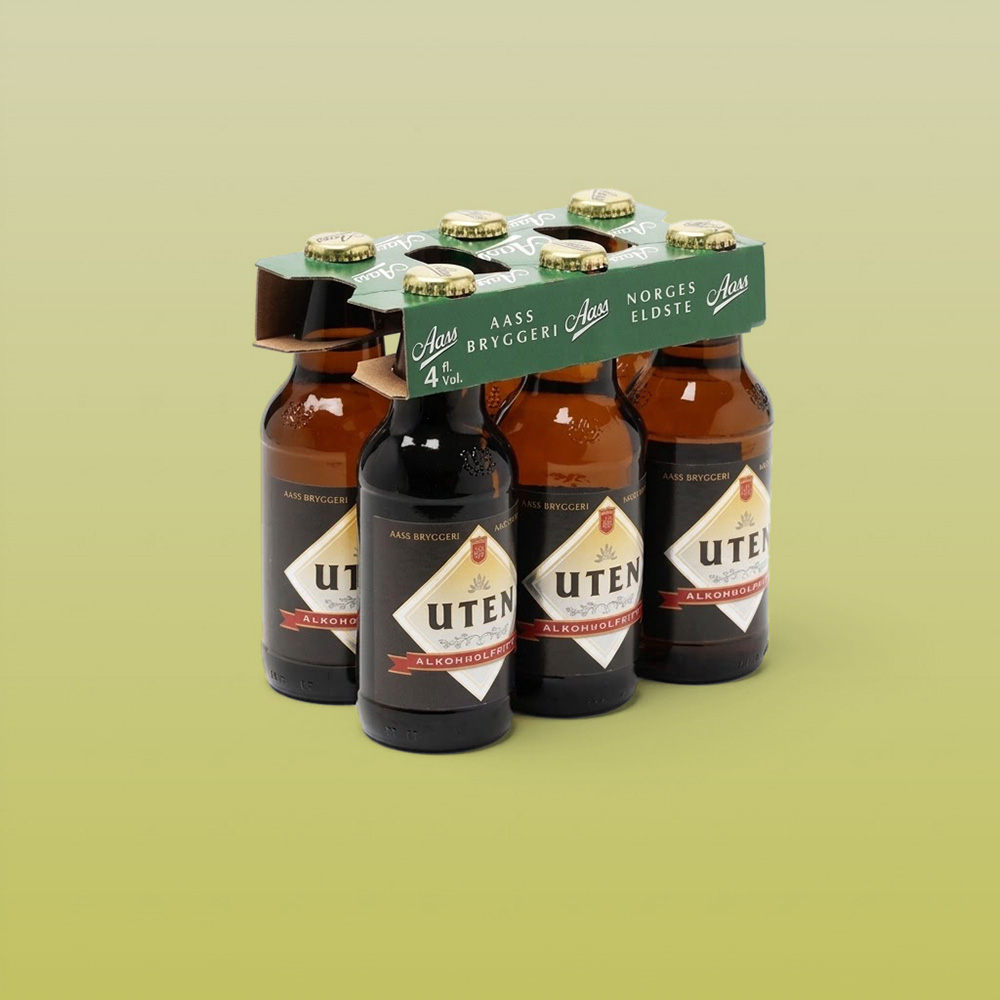
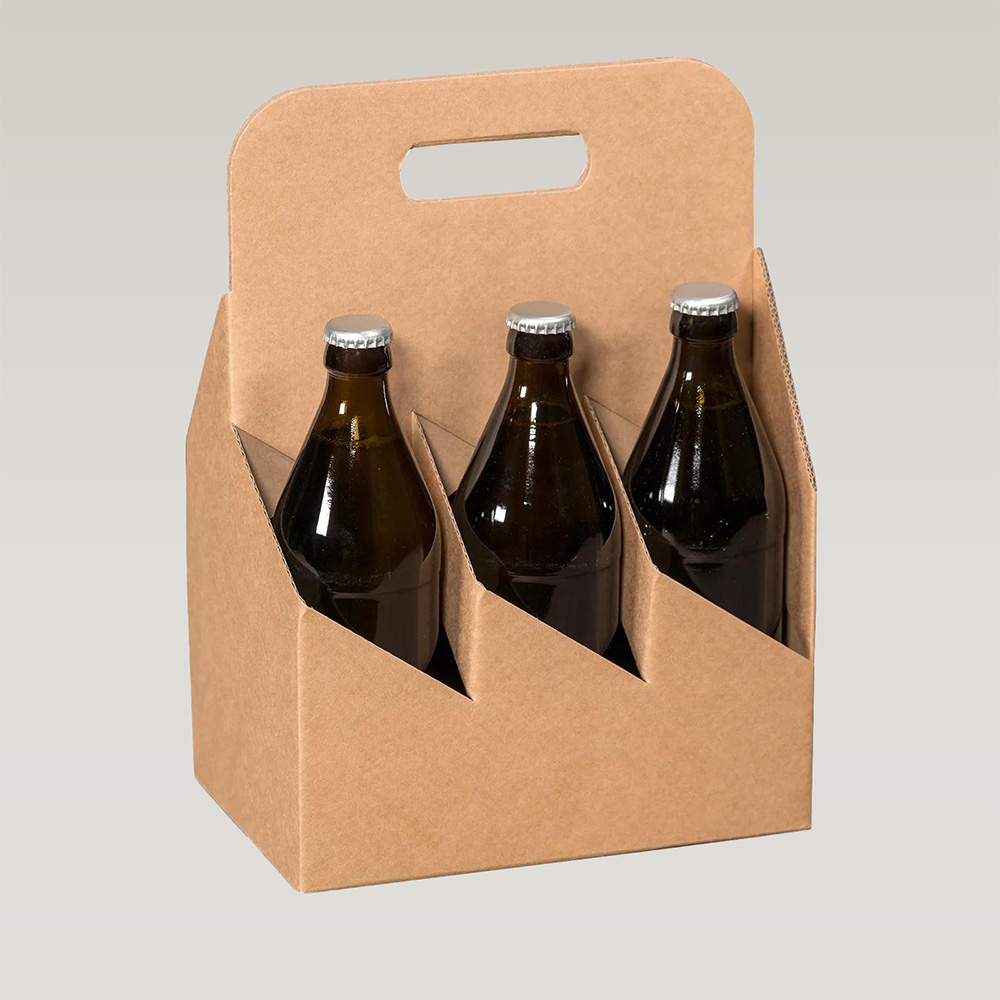
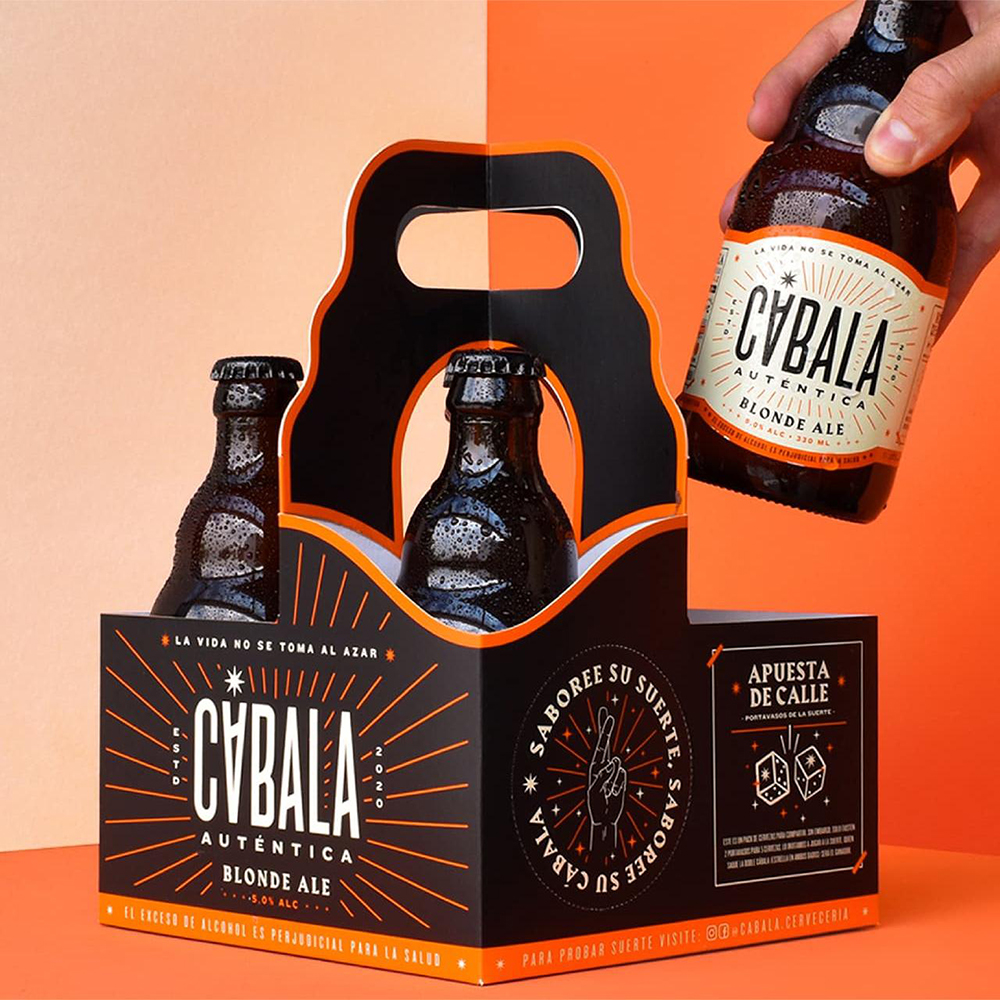
A can multipack has a longer road ahead of it than most people realise, from the packing line all the way to a customer's fridge. Hale Path Packaging builds custom can multipack packaging for beverage brands across the USA, and we size every can carrier box to the exact can diameter and weight going inside, not a roughly close size.
Showing all 7 resultsSorted by latest
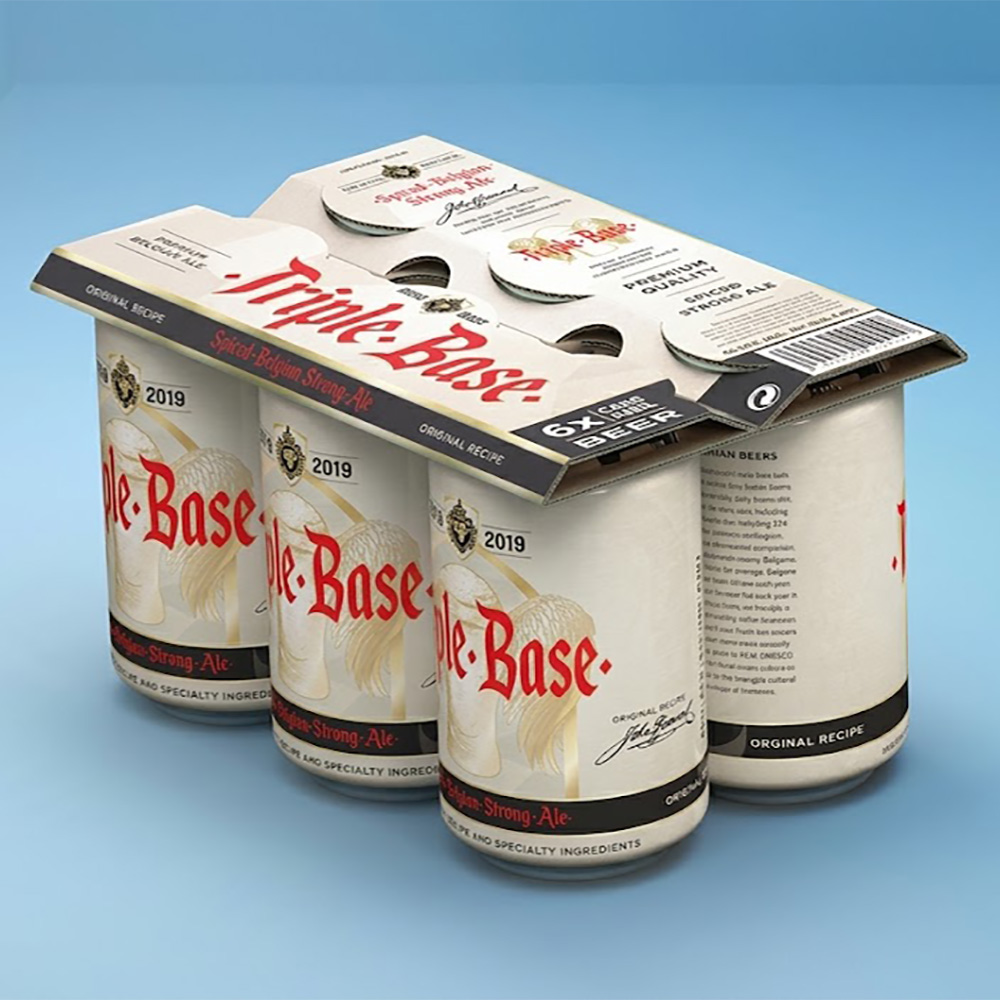
A multipack carrier usually gets judged on one thing: how it looks sitting on a shelf, but that’s really just the final moment in a much longer story. Before it ever gets there, it’s gone through a packing line, a pallet, a shipping route, a stretch in storage, and a restock by someone who had thirty other things to do that shift.
The Hale Path Advantage for Can Multipack Packaging
Everything is made in-house, from structural design to the print on the outer wrap. We don’t outsource printing to a separate shop, which cuts down on the handoffs where a colour or die-line can drift between the approved sample and the shipped batch.
We work with craft beverage producers in Austin and soda bottlers in Chicago, and the can size question comes up most for both a standard beer can carrier and a soda can multipack. Try putting a 16-ounce can where a 12-ounce one used to go, and the carrier won’t hold up the same way, even with the same number of cans inside. We build the cavity around the exact can, with the same precision behind our Custom Rigid Boxes USA line.
Print durability comes up often too, especially for cold or refrigerated product. Standard inks can stain when a carrier is handled wet, so we match coating and ink choice to how the product is actually going to be taken.
Get Custom Quote
A soda bottler in Chicago switched from a 12-ounce can to a taller 16-ounce can and kept using the existing carrier mould to save time. The taller cans shifted the pack’s weight higher than the original design accounted for, and carriers started splitting at the handle during a routine one-handed lift off a pallet.
We resized the carrier for the new can dimensions and reinforced the handle point to match the real loaded weight, then tested it against the same one-handed lift that caused the original failures. Handle failures dropped to almost none in the next production run.
Two multipacks with the same can count can put very different stress on a handle, depending on can width and weight. Treating every multipack the same, regardless of can size, is the most common reason a handle design fails on a different product. That’s the same load-specific thinking behind our single Wall Boxes USA builds for heavier products.
Most multipack failures trace back to a can size change that wasn’t matched with a new carrier spec. We now treat every can size change as its own design question, not an assumption that an old mould still fits. That same thinking carries into our Bottle Carriers Packaging USA work too.
Our Tri-Wall Corrugated Boxes USA line covers larger liquid formats. Our Plastic-Free Carriers Packaging USA team can build a paperboard choice for brands moving away from plastic rings.
Get Custom QuoteNot reliably. A taller or wider can turns weight and pressure differently, so each size requires its own transport spec.
It can, without the right layer. A condensation-resistant layer saves it from softening when cans are cold.
Can weight counts more in most cases. A 6-pack of broader cans can underline a handle more than an 8-pack of narrower ones.
Can diameter, can height, pack count, and whether the product is crafted cold or ambient.
Plan on two to three weeks after the artwork is approved.
They are, as long as they are constructed from standard paperboard without a heavy plastic lamination.
Excellent services! They helped choose the right size, finish, and window shape. The boxes fit our brand, and the minimum order quantity was reasonable for business.
They helped us pick the right size, finish, and custom window shape. The boxes fit our brand perfectly, and the minimum order quantity was reasonable.
We wanted luxury but eco-friendly. They suggested recyclable rigid boxes with a frosted window and satin insert. Customers now post unboxing videos; that’s how good they look.
We needed custom boxes with a logo and food-safe window for our Eid cookies. They guided us on materials and delivered exactly what we wanted. Clients love the unboxing.
Highly satisfied with Hale Path Packaging. Their packaging solutions were premium, printing was vibrant, and their high quality and customer happiness made them a trusted partner.
Hale Path Packaging delivered unique packaging products. The boxes were sturdy, printing was vibrant, and their attention to detail ensured products looked premium in the market
They provided reliable and high-quality packaging solutions. The boxes and pouches were well-designed, printed perfectly, and delivered on schedule with excellent customer support throughout for brands.
Hale Path Packaging impressed us with their boxes and pouches. The printing was perfect, materials were durable, and their team handled everything efficiently with excellent service.
Outstanding experience with Hale Path Packaging. Their packaging solutions were durable, beautifully printed, and delivered on time. The team was responsive and ensured a happy order.
Hale Path Packaging delivered high-quality packaging materials with perfect printing. Their attention to detail and deadlines made them a trustworthy partner. Our customer was really satisfied.